We previously discussed, Best Practices: Machinery Alignment Shimming Part I. In this blog, we discuss shimming techniques, choosing the right shims to use, and more.
Note: This blog post is an abridged version of a longer article on this subject published by the author in 2013.
SHIMMING TECHNIQUE
Always sandwich your thinner shims between thicker ones to protect them. In fact, if you have to shim 26 thousandths, choose to use a 20 and two 3s, rather than a 25 and a 1 alone.
Always insert your shims until you feel them touch and then withdraw them slightly. This way you know for sure that you are not letting the slot of the shim get caught in the threads of the anchor bolt.
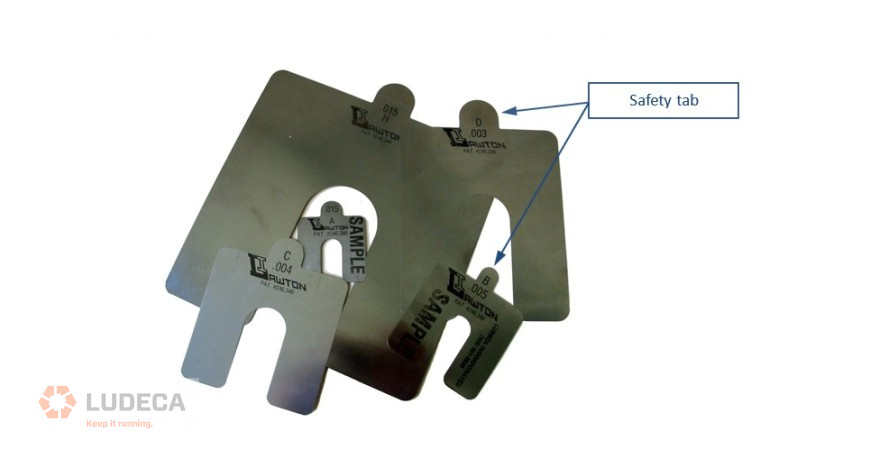
Always handle your shims by grasping them by the safety tab (see Figure 1); never let your fingers get under a machine foot while the machine is being pried up or lifted!
CHOOSING THE RIGHT SHIM TO USE
You can choose your shim size by the horsepower of the machine; however choosing by the slot size is fine too. The foot’s surface area is less important. It is a myth that you have to support the entire surface area of the machine foot with the shim. You only need to support the load zone around the anchor bolt. See Figure 2 for an illustration of the load zone and the area that should be supported by the shims. Most machine feet are made much larger in surface area than what is strictly necessary to support the mass of the machine and its operational load stresses. So, if a machine foot is larger than a given size of a shim, but the shim adequately supports the load zone around the hole in the foot, you do not have to worry if the outer edges of the foot overhang the shim a bit—that is perfectly okay.
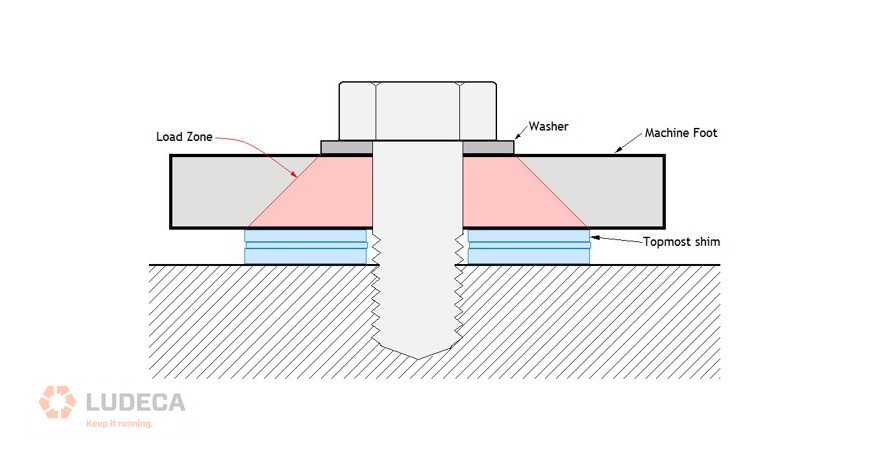
The load zone (depicted in red) is defined as a cone approximately 45 degrees from the edge of the flat washer under the anchor bolt through the thickness of the machine foot. As long as your topmost shim supports the surface area defined by the cross-sectional cut of this cone under the foot, you are adequately supporting the load zone of the machine’s foot and do not need to support any excess surface area under the foot.
SHIMMING MISTAKES
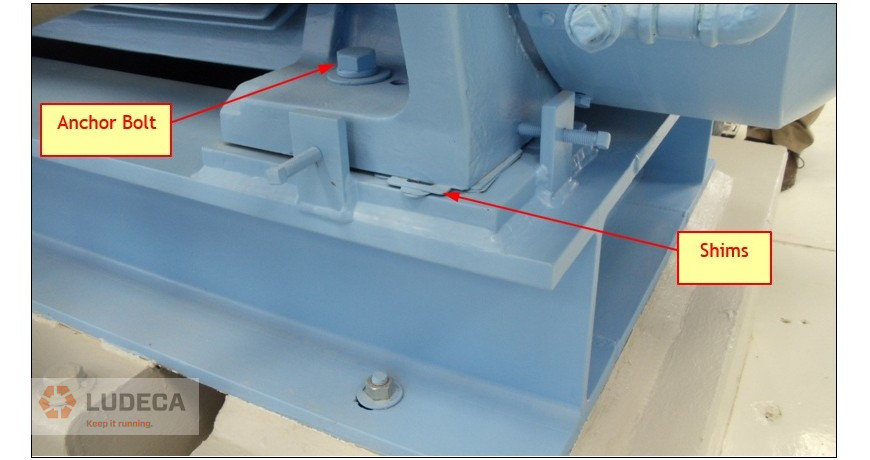
Figure 3 shows an example of how not to shim a machine: Too many shims were used and the shims do not support the load zone of the machine’s foot around the anchor bolt. Moreover, the Size ‘A’ shim used on top of the shim stack is too small for a motor of this size. When the anchor bolt of this foot is tightened, the foot will be stressed, distorting the machine’s frame and altering the internal alignment of the bearing bores, as well as affecting the air gap between rotor and stator. Note too that the motor was painted in situ, covering the shims and jackscrews in paint and also allowing paint to get under the foot. These are all bad practices.
UNUSUAL CIRCUMSTANCES: STEP-SHIMMING
Sometimes, a machine will have feet that are significantly angled with respect to the contact surface of the base plate or sole plate supporting them. This can be caused when the feet are accidentally bent, or when the machine is “rolled” to accommodate a horizontal misalignment problem (definitely not a best practice!) Tightening the anchor bolts under these conditions would force the feet flat to the base, thereby distorting the machine and increasing the radial load on the bearings. This affects air gap clearances between internal components and places undue stress on the feet or other machine parts. How do you solve this problem? The best way, of course, would be to re-machine the base plate, sole plate, or undersides of the machine feet in such a way as to eliminate the lack of coplanarity. However, this may not be practical or economical to do. This leaves us with the only other possible solution: step shimming.
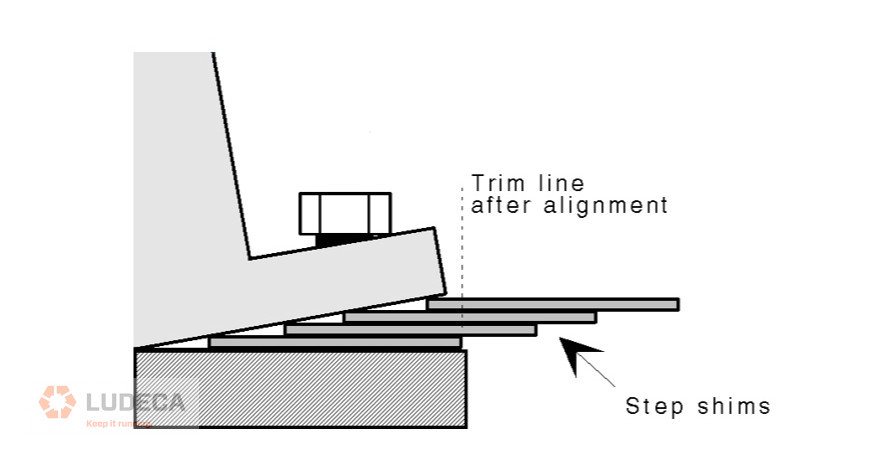
Step shimming requires several thinner shims to be carefully inserted between the machine’s foot and its support surface in such a way that they are offset from one another in step fashion. This fills the tapered gap between the underside of the foot and its support plane as evenly as possible, as illustrated in Figure 4. This may require you to use more than three shims overall, but as with everything, there is always an exception to the rule and here the benefits of doing this outweigh the disadvantages. Although not elegant, the step shimming solution is expedient, easy and economical, and will prevent a much more serious problem resulting from machine frame distortion, allowing your machines to run satisfactorily until your next major outage.
The angles illustrated in Figure 4 are vastly exaggerated to illustrate the concept. It goes without saying that we are talking about angles with a rise over run of just a few thousandths of a inch per inch. To step shim correctly, choose a shim thickness that will allow you to stack no more than four shims to fill the uneven air gap between the underside of the foot and its support surface. Step shimming works well since the angles involved are sufficiently small enough to fall well within what is known as the ‘swedge’ angle for the coefficient of friction of the materials involved. This means as you tighten the anchor bolts and apply load to the shims, they will tend to remain in place rather than “squirt out” like watermelon seeds. Once the step shimming task is complete and the alignment of the machines has been rechecked with all anchor bolts tight, do not neglect to trim off the excess part of the shims protruding out from under the edge of the machine’s foot to prevent possible injury.
It also goes without saying that if the time and resources are readily available, you should consider re-machining the undersides of the feet or the contact surfaces of the base plate, or making a tapered “dutchman” shim for the foot. Keep in mind, too, that the “bent” foot may be symptomatic of a larger problem with the machine, such as internal damage if it resulted from the machine being dropped in transport or installation. If the angularity between the foot and the base is too large, consider replacing the entire machine or the base, as may be. ª
Download our Shimming Best Practices infographic for an outline of 7 things to consider when using shims for machine installation or machine alignment plus Step Shimming!
by Diana Pereda
When using a laser shaft alignment system, one of the most important things to understand is how the laser adjustment wheels work. These wheels allow you to move the position of laser dot on the detector to place it where you need it to take full advantage of the detector’s range. The laser dot does not necessarily need to be in the center of the detector when you begin your measurement.
Think of it the same way you would use a dial indicator. We don’t always place the plunger exactly in the middle of its travel range as this may limit our measurement in either direction. Depending on the situation, we may intentionally position the plunger farther in or farther out so that we have enough usable travel range to measure the movement we expect.
The same principle applies to the adjustment wheels on a laser alignment system. We use them to strategically position the laser dot where it needs to be to allow us to measure the misalignment. Understanding this concept allows technicians to get the most out of the measurement system and, more importantly, avoid limiting the measurement range of the detector unnecessarily.
The image below illustrates how a dot on the bottom right is ideal if the misalignment moves the laser dot to the left and up:
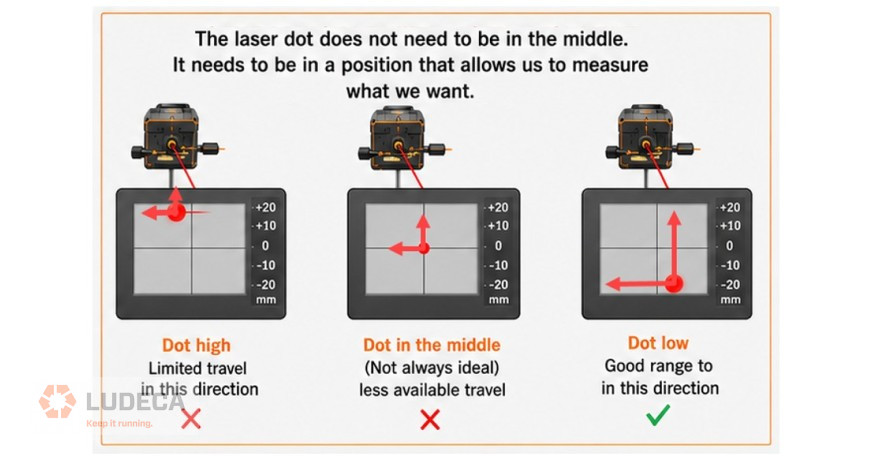
Use the adjustment wheels as a tool to help—not just to center the laser!
As you begin turning the shafts, carefully observe which way the laser dot travels on the detector. Then, next time around, you can deliberately readjust the laser’s position in the opposite direction by as much as possible, in order to maximize the travel range of the beam as you turn the shafts again. This little trick might save the day in allowing you to obtain enough shaft rotation to get good readings, whereas when you start centered you might run out of range too soon and not get reliable readings.
I use a Laser Alignment System, so I am Performing Precision Alignment, Right?
by Diana Pereda

Note: This blog post is an abridged version of a longer article on this subject published by the author in 2013.
There is much more to proper shimming of machines for alignment than meets the eye. There are a number of things you should consider when selecting and using shims.
First and foremost, you should be using high quality, precut slotted stainless steel shims. Cutting your own shims by hand out of cheaper rolls of carbon steel or brass shim stock may save you money in materials, but will prove far more expensive overall for several reasons. For one thing, you will be able to cut only the thinner thicknesses with scissors or shears, whereas thicker thicknesses (over 0.004″) will require using an acetylene torch or a saw, which is labor intensive and presents several safety concerns. After you have cut your shims by hand, it is essential to deburr them carefully with a ball peen hammer and file. All of this will cost you the most valuable commodity of all: time. Moreover, the end result will be fewer available shim thicknesses than you would otherwise have with precut stainless steel shims, resulting in less precise alignments. In addition, if you are cutting shims by hand, there is a far higher risk of minor cuts, requiring a visit to the nurse for a bandage, with all the attendant loss of time and safety reporting paperwork that this would entail.
It is important to select your brand of precut stainless steel shims carefully, as they vary widely in quality and tolerances. It is extremely important that the shim be of consistent quality, completely even in its thickness throughout, accurate in its thickness, flat, and burr free. Also, it should have no hazardous sharp edges. The metallurgy of the shim is also important, to guarantee its hardness and corrosion resistance. Only the best quality precut stainless steel shims offers all of these features. An excellent shim will always save you time and money in the long run. Let’s see why:
ADVANTAGES OF PRECUT STAINLESS STEEL SHIMS
Precut stainless steel shims are:
- Precut: You don’t have to hand cut them, saving you much time.
- Burr free: This means greater precision in the thickness.
- Accurate in their thickness (up to 0.025″.)
- Even thickness throughout.
- Flat and undistorted.
- Convenient: Handy steel carrying cases make transporting shims easy and help to keep them neat and organized.
- Versatile: More thicknesses and sizes to choose from means you will use fewer shims to achieve the desired thickness, thereby saving both time and money in materials.
- Safe: The safety tab allows for safe manipulation of each shim. Never allow your fingers to get under a machine foot!
Some of these points require further attention, as they have a direct impact on your best practices regime. Let’s examine a few of these.
NUMBER OF SHIMS
First, you should try to never use more than three (or four at most) precut shims under one machine foot, except in exceptional circumstances. The reason for this is that too many shims under a machine foot leads to increased risk of exceeding your permissible soft foot tolerance. This effect is usually due to a slight lack of coplanarity between the machine’s feet and base, and in some cases, slight bowing of the shims. If you add to this the effect of surface contaminants present on both faces of each shim (finger oils, dust, grease, etc.), the movement can be greater.
Limiting your shimming to just three shims under a machine foot is best good practice. Good machine installation practices dictate that a good rough alignment between the machines should not necessitate ever having more than 100 mils worth of shims under any machine foot to achieve a final alignment within tolerance. Good quality, precut stainless steel shims come in 13 thicknesses, ranging from 1 mil to 120 mils. By combining these 13 thicknesses, you can achieve any desired shim thickness, from 1 to 150 thousandths, with never more than three shims.
This saves money since a greater variety in available thicknesses means you almost never need to use more than two, or at the most three, shims under one machine foot. Over time, this adds up to a lot of saved shims. As part of this best practice, it is imperative that you always maintain your shim cases fully stocked with all thicknesses, otherwise shim consumption may balloon. For instance, if you run out of fifteens, you will find yourself using a ten and a five, or three fives, which quickly escalates your shim costs and increases the risk of violating the rule of using no more than three shims under a foot.
If you absolutely must shim your machine up by more than 150 thousandths, then go ahead and use four shims; however, if you must shim up 0.250″ or more, then have your machine shop make you a chock (a chock is any shim that is 250 mils or more in thickness) and make sure this chock is carefully milled flat and coplanar on both faces. Then use three or fewer shims, normally on top of the chock, to complete the alignment.
ASCERTAINING PRECISION OF SHIMS
Always measure the thickness of any shim 0.050″ or thicker with a micrometer. While an excellent quality shim is even in its thickness throughout, like all commercial precut shims, it is only guaranteed accurate in its marked thicknesses from 0.001″ to 0.025″. Thicker thicknesses are always nominal (just as the steel mill rolled the sheet) and should therefore always be miked. For instance 0.075″ shims may mike out at 0.078″, and 0.100″ shims may actually measure 0.104″ thick. This does not matter, so long as you know it! Thus, make sure a 1″ micrometer is a standard part of your alignment toolkit.
MARKING AND QUALITY OF SHIMS
Always prefer precut stainless steel 304 shims whose thickness and size are indelibly etched upon them. This is a sign of a best quality shim. Avoid using cheaper brands that only ink their shims, or worse yet, punch stamp them with the thickness marking. Punch stamping the thickness on shims ensures that they are not flat, resulting in a leaf spring effect under the machine feet that contributes to a “squishy foot” soft foot.
Some lesser quality shims usually have raised knife edges (burrs) along their edges because they are not tumbled after being stamped out of the sheet and the dies used to stamp them out are not sharpened often enough. This also results in a shim of inaccurate thickness which will contribute to or even cause a squishy soft foot; it also constitutes a significant safety hazard for the millwright who is not using safety gloves.
MYTH or TRUTH? All Soft Foot Conditions can be Corrected by Proper Shimming
by Diana Pereda
Calculating the total cost of laser alignment requires looking far beyond the price tag on the equipment itself. The initial investment in a laser shaft alignment tool is just one component. And often, it’s not even the most significant one when you factor in the operational budget over the machine’s lifecycle. The real costs are hidden in unplanned downtime, excessive energy consumption, and premature component failure.

Beyond the price of laser alignment equipment
The initial purchase of laser alignment equipment can range from a few thousand to tens of thousands of dollars. But this capital expenditure is a single event. A cheaper system might seem attractive, but it can lead to higher long-term costs due to less accuracy, a steeper learning curve for technicians, and a shorter lifespan. The investment should instead be weighed against the repeated, compounding costs of not having precision alignment capability.
The hidden expense of poor machine reliability
Misalignment is a primary cause of catastrophic machine failure. It directly leads to increased stress on bearings, seals, and couplings, which are the components that keep machinery running. So when a bearing fails unexpectedly, the cost isn’t just the replacement part. The true cost is the lost production, the man-hours for the emergency repair, and the potential for secondary damage to other components. Proper alignment drastically improves machine reliability, turning reactive emergency repairs into predictable, planned maintenance activities.
Download our 5-Step Shaft Alignment Procedure which provides a simple and effective procedure for shaft alignment of rotating equipment.

The impact on energy consumption
A misaligned shaft forces the motor to work harder to overcome internal friction and resistance. This increased load directly translates to higher energy consumption. Even a slight misalignment can increase power draw by several percent, which, across multiple assets in a large facility, accumulates into a significant operational expense on the utility bill. Precision alignment minimizes this waste, allowing the machine to operate at its designed efficiency and reducing the strain on the motor.
The connection between alignment and vibration
Vibration analysis is a critical diagnostic tool for assessing machine health. But one of the most common sources of harmful vibration is shaft misalignment. Performing routine vibration analysis will certainly detect the problem, but it doesn’t fix the root cause. A proactive alignment program prevents the vibration from occurring in the first place. This reduces the need for constant monitoring and reactive troubleshooting, freeing up maintenance resources for other tasks and leading to a quieter, more stable operational environment.
The value of professional alignment services
Not every facility has the need or the budget for in-house laser alignment equipment and trained personnel. This is where professional alignment services become a variable cost instead of a capital one. Outsourcing the task provides access to expert technicians and high-end equipment without the upfront investment or ongoing training costs. For critical or complex laser shaft alignment jobs, using a specialized service can be far more cost-effective than attempting it with less experienced internal staff. However, many times having your own equipment and also investing in alignment training for your staff means you are in full control of how and when to do preventive maintenance.
Reducing long-term maintenance costs
Ultimately, precision laser alignment is a tool for reducing overall maintenance costs. By eliminating a primary root cause of failure, you extend the life of bearings, seals, and couplings. This means fewer purchases of spare parts, less labor spent on replacements, and a more predictable maintenance schedule. The cost of an alignment program is easily offset by the savings generated from avoiding just a few major component failures per year.
Therefore, the real cost of laser alignment isn’t what you pay for the tool or the service. It’s determined by how much you save by preventing costly failures, reducing energy waste, and improving the overall reliability of your plant’s machinery. The calculation must include every factor, from downtime to energy bills, to get a true financial picture.
Thank you Easy-Laser for sharing this informative article with us!
by Diana Pereda
One of the problems that we encounter with belt-driven machinery is shortened belt life. Listed below are the most common reasons for shortened belt life and some advice on how to avoid these problems.
- Excessive belt stretch: This is a result of misaligned sheaves, a broken tensile member in one belt, or a significantly overloaded drive. Using a precision laser belt alignment tool for aligning the sheaves will eliminate the misalignment problems. Taking the time to properly install the belts by loosening the adjustment and not rolling the belts on under heavy tension will lessen the chances of broken cords in the belt. Proper tension is generally considered to be 1/64″ of deflection (or “give”) per inch of span length when pressed with a spring scale to the belt manufacturer’s recommended amount of force.
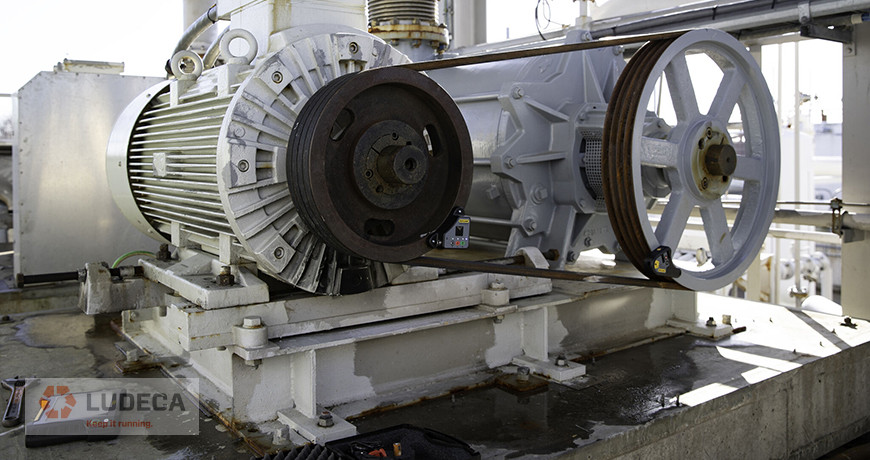
- Worn sheave grooves: For V-belt sheaves inspect the grooves for wear and nicks. Place the proper sheave gauge into the sheave groove and check for wear. If more than 1/32″ of wear can be seen between the gauge and groove side wall, the sheaves are worn and should be replaced. Do not be misled by “shiny” grooves. Grooves that are shiny are often polished because of heavy wear. Inspect the sheave grooves for rust or pitting. If either is found, then replace the sheave. For Synchronous sprockets — Inspect sprocket grooves for unusual or excessive wear. Check for excessive wear by both visually inspecting the grooves and by running your finger along the sprocket groove (using proper PPE to avoid injuries). If you can see or feel noticeable wear, replace the sprocket.
- Oil or grease on belts make the belt side-walls sticky or swell the belt’s cross-section: Use proper guarding to protect the belt and sheaves as well as avoid over lubricating machinery.
- Belts rubbing against guards and frames: Ensure that the guards are fabricated to the correct dimensions to avoid rubbing. You should also inspect the guards for damage.
- Incorrect sheave size: Sheaves that are too small may cause the bottom of the belt to crack.
- Dirty and dusty sheave grooves: cause belts to track poorly, whip, and vibrate. Squeaking and chirping noises are usually associated with dirty sheave conditions. Do not apply belt dressing or oil to the belt to eliminate the noise. Instead, address the underlying root cause of the problem.
Download our Pulley Alignment Guide plus 5-Step Procedure for information on the implementation of good pulley alignment of belt-driven equipment including terminology, alignment methods, belt maintenance, storage and tensioning as well as a 5-Step Sheave/Pulley Alignment Procedure.
by Diana Pereda
Reliability professionals have often asked us whether laser shaft alignment systems measure using the “rim and face method”. The question is understandable because results are typically reported as offset (radial separation of shaft centerlines at the coupling) and angle (angular misalignment, sometimes expressed as gap difference across the coupling faces). These values are compared to industry tolerance tables such as ANSI/ASA standards to determine if alignment is acceptable. Understanding the evolution of alignment techniques clarifies how today’s laser tools work and why they do not rely on the traditional rim and face approach.
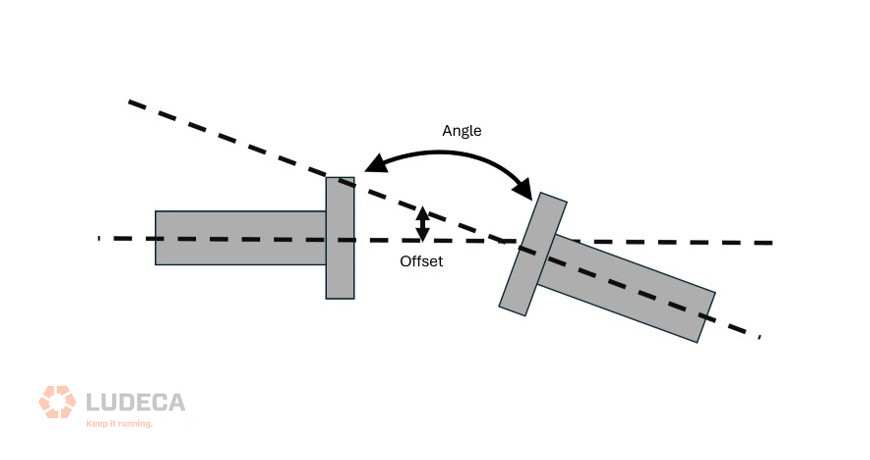
The earliest methods used simple mechanical tools. A straight edge was placed across the coupling rims (top and sides) to check for parallel offset. If no light showed underneath, offset was considered corrected. Feeler gauges measured gaps at multiple points around the coupling face to detect angular misalignment; equal gaps indicated parallel faces. Adjustments were made by shimming or moving machines until both offset and gap fell within acceptable limits. While this gave a basic starting point, it lacked precision and repeatability due to variations in feel, tool placement, and surface irregularities, not to mention that the positioning of the coupling itself was not guaranteed to be exactly with the shaft centerlines of rotation.
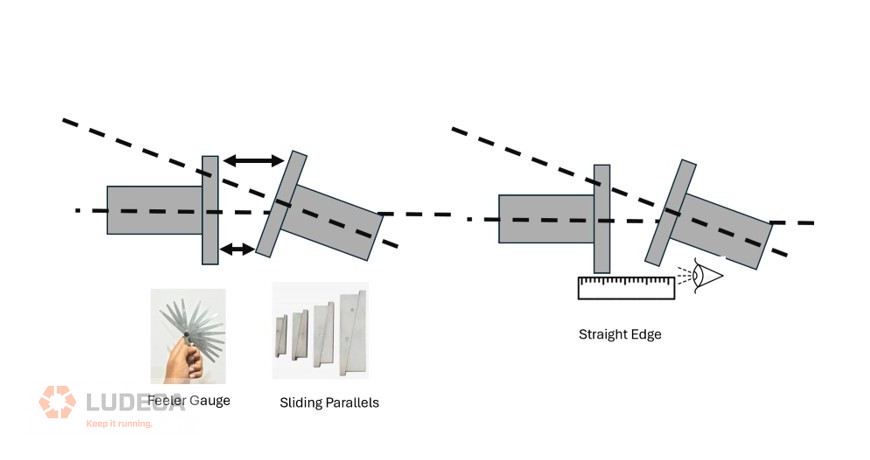
As practices advanced, the rim and face methods with dial indicators became popular. One indicator measured rim offset while another on the face captured angular changes as the shafts were rotated together. Rotation physically cancels surface imperfections such as nicks, burrs, or coupling runout. This provided numerical results and better accuracy than straight edges and feeler gauges. However, axial float or end play in the shafts often introduced errors in the face readings, requiring repeated measurements and careful calculation.
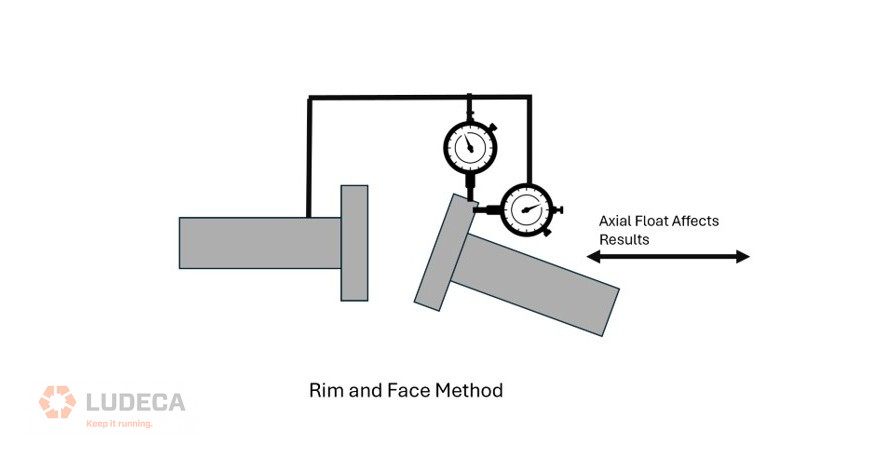
Speaking of calculation, I rarely saw calculations or graph paper being used for dial indicator alignments in my interactions with various facilities. Perhaps this explains why the rim and face method remained popular—it was much easier to conceptually visualize the alignment based on the dial indicator readings alone. Simply taking the Total Indicated Runout (TIR) /2 of the rim readings would give you the shaft offset. Take the gap reading and note the coupling face diameter—that was your angle, for which you could use a multiplier based on that coupling value to figure out the shim corrections. Experienced professionals could and often did literally do that in their heads. Not everyone had that skill, thus computers came into the picture to make that task easier.
A more reliable solution emerged with the double dial indicator (reverse rim) method. Instead of measuring the face directly, two rim readings are taken at opposite sides of the coupling, spaced some distance apart along the axis of the shafts. Using half the total indicated reading (TIR) and the distance between measurement planes to the coupling center, technicians could calculate both offset and angle. This approach largely eliminated errors from axial play.
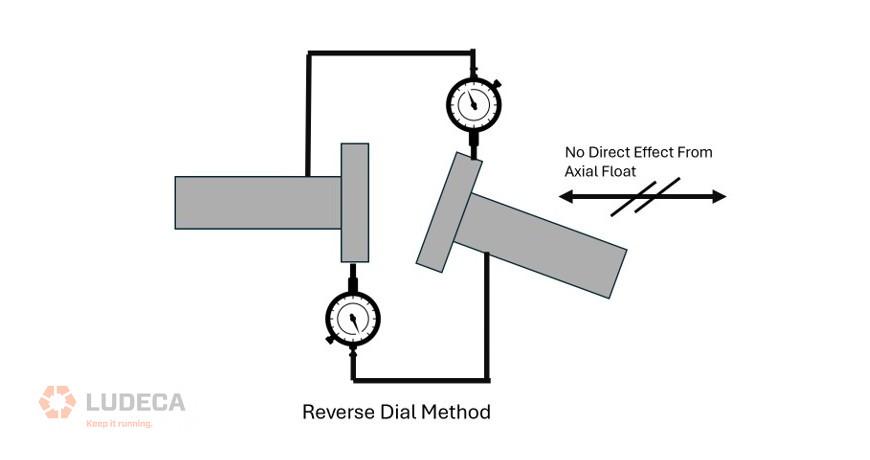
Modern laser alignment systems, such as the Easy-Laser XT770, build directly on this double offset principle. They use laser beams and position-sensitive detectors (PSD)—essentially highly precise, non-contact “dial indicators.” Whether using dual laser/detector setups on both shafts or a single laser with fixed detector positions, the systems capture a minimum of three sets of offset readings at different rotational angles.
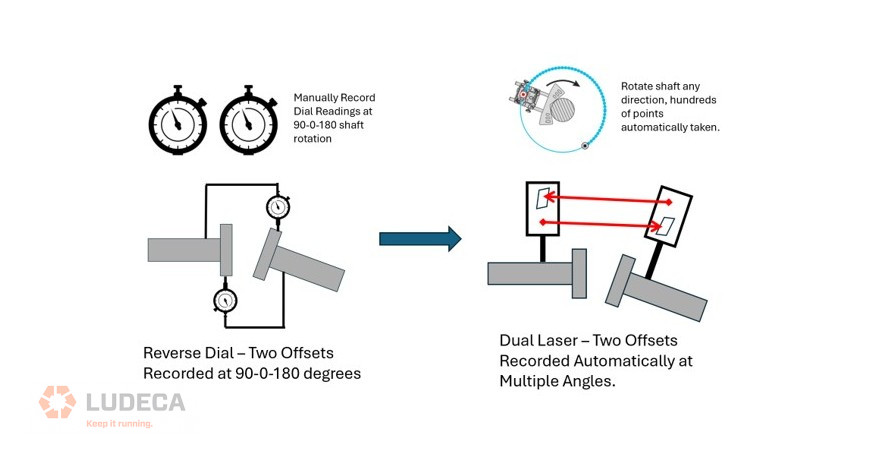
The best, such as Easy-Laser, capture hundreds of sets of readings for accuracy assurance in field conditions. Software then converts these into the familiar offset and angle (or gap) values for tolerance comparison. In addition to higher measurement resolution, key advantages include eliminating mechanical linkages and bar sag errors (typically 10-20 mils or 0.25-0.5 mm if overlooked) while automatically handling calculations.
By appreciating this foundation, reliability teams can better understand how laser tools enhance precision alignment practices, reduce training expense, reduce unplanned downtime, and support long-term asset health—core elements of effective maintenance programs.
by Diana Pereda
It has been almost exactly a decade since I was laid off from my job in the gas industry. It was an abrupt change to my life, both emotionally and professionally. I knew things were headed downhill with the company where I worked but I thought our department’s value to the company was nationwide, not just the region where we were based. Unfortunately, real estate deals do not see offices in that light. Our building (and the jobs being performed there) were part of a complete market sell-off. I was taken by surprise, but I can’t say I was completely shocked. I was given a severance and insurance benefits, so I had the luxury of waiting a bit for the right job to come along. That doesn’t mean that I was sitting idle. On the contrary, I definitely was on the hunt for another job. It didn’t have to be just any job, but one that I could be secure with and maybe even grow a bit more professionally (well, kind of. If you know me, you know the challenge there).
One of the jobs that popped up was as part of the training group with Ludeca. I knew about Ludeca from the past, since we had bought laser alignment kits from them in the past. They knew me from the department I had been part of, and what kind of curriculum we used for corporate training and industry meetings. We talked about things a lot before either side said “yes”, and I have to admit that I felt a bit of pressure coming into the job. I would be working with not just one industry, but all industries. And I would be working in a group of engineers, not just tradesmen and mechanics. I needed to step my game up BIG TIME if I was going to swim in these waters. Ludeca also works with different technologies than I was used to, so I needed to learn and understand how those tools worked and what kind of applications called for which technologies.
Here are the take-aways from that learning curve and my continued education working with a technology-based company:
-
You don’t know what you don’t know.
I feel like I had a pretty firm grasp on things. I had been a mechanic most of my life. With years of different fields of turning wrenches, I figured I could catch on pretty quickly. WRONG! Some types of work we do require constant practice and learning to stay abreast of what is being done with not only the current crop of tools being used, but also the evolution of those tools as the market evolves as well.
-
Check you ego at the door but bring your experience with you.
Even having a ton of credentials doesn’t make you an expert on anything. They provide you with a basis for evaluation of the facts, and sometimes even clarity you might have been lacking before. I see so many issues from my past life that I would address differently if I had a chance to do it over again. What I know now would have made my life so much easier. For example, we were fighting a vibration issue with a compressor. Based on the advice of someone with no vibration experience, we kept working on the problem as if it was all from a bad alignment. If we knew how to look at the vibration data, we would have focused our energy on the gas flow issues that caused the vibration instead of assuming vibration is only caused by alignment. My goal now is to share that clarity with those who are still doing the tasks I did and maybe make their jobs easier.
-
Always ask “Why”
Knowing the “why” makes it easier to understand the task and the desired outcome for that task. So many techs are told to do something in just such a way and given no real explanation as to why it’s being done that way. Asking “Why” should establish a clear path to completion, and if it does not work out maybe we readdress what is being done to more closely align with the desired results. Doing a task with nothing but “because” does not add value to that task. At that point, it is just checking things off of a list.
Which leads to one of the biggest things that I have learned since working for Ludeca.
-
Know where to find your specifications and check them continuously.
We had so many numbers thrown at us in Gas Compression, and most of them were hand-me-down knowledge from a long time ago. I was aware of this when I was in the field, and I even got a much better understanding of this when I went into training. A lot of that data was corrupted by things like individual experience, or back to the “because we said so” working habits. Sometimes there are changes to a certain product or specifications to get a better result, but if we always adhere to the hearsay, we might never achieve that result. I have grown past the point of memorizing numbers. I work on knowing where to look them up, and I also try to look for the newest data for those specifications in case they have been updated.
There is a ton more I have learned working for Ludeca, which could last for much longer than just a blog. Things like vibration, where I have been able to work my way up to a category 2 certification. It has changed my view on machinery just as much as the Failure Analysis class I had in 2011. Ultrasound tools are something we looked at back in the days of compression, but we didn’t understand how it would work in our loud environment. Now, we have not only the ultrasonic inspection tools to “hear” the issues, but the ultrasonic imagers that let us “see” the noise and the source. The induction heaters we carry would have saved us so many issues with hub installation, and we could have done it at a safer pace than trying to handle a 300 pound part that was just getting hit by four torches at once.
I have come a long way from just talking about that “.005″ for offset and .005″ for angularity” tolerance for compression alignment. And that was all we looked for with our dial indicators. Knowing how much we didn’t know about alignment means that maybe we should have another talk about that “5 and 5” and come up with better tolerances for that kind of equipment. It might just make your life easier, or at least give you some clarity.
Three Things Leaders Can Do to Impact Condition Monitoring and Precision Maintenance Programs
by Diana Pereda
The phrase “Measure Twice, Cut Once” emphasizes the importance of careful planning and verification to avoid costly mistakes. Here’s why it’s good practice:
- Prevents Waste: Double-checking measurements ensures accuracy, reducing the chance of adjusting incorrectly and wasting resources.
- Saves Time: Taking a moment to confirm measurements upfront avoids the need for rework or starting over, which can be time-consuming.
- Improves Quality: Precise measurements lead to better corrections, resulting in higher-quality and precision alignments.
- Builds Confidence: Reliable, repeatable results instill trust in the alignment process and tools, just as careful measurements build confidence in a craftsman’s work.
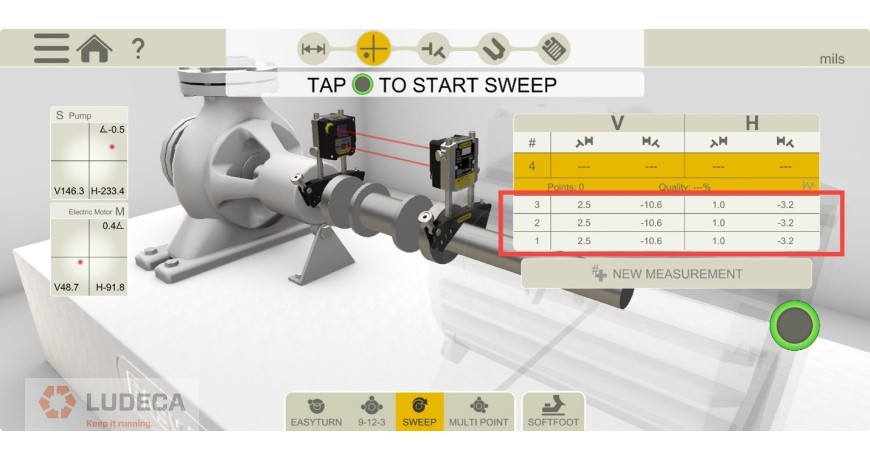
Your laser alignment system should have an easy to find and accessible table of measurements on the measure screen, allowing you to easily compare readings. For example, sweeps 1, 2, & 3 from the image below repeat perfectly. In laser shaft alignment this repeatability, the alignment readings should repeat with 1 mil of each other for excellent repeatability.
Tips for Achieving Repeatability:
- Rotate Consistently: Take measurements rotating in the same direction and at constant speed each time to minimize variability.
- Calibrate Regularly: Periodic calibration of the laser system ensures measurement reliability. Send units to certified calibration centers as recommended by the manufacturer.
Watch our Shaft Alignment Know-How: Repeatability to learn the importance of achieving repeatability of measurements before making alignment corrections.
Shaft Alignment Measurement Mode: 9-12-3 The Classic Three-Point Method
by Diana Pereda
Correct shaft alignment is a critical part of ensuring machine reliability, performance, and energy efficiency. Whether you’re working with a simple pump/motor unit or a complex machine train, precision alignment reduces wear, lowers vibration levels, and extends equipment life.
Today, laser alignment systems make the job faster and more accurate, and they can adapt to a wide range of machine setups. In this article we’ll take a closer look at how the Easy-Laser alignment systems handle different machine configurations: horizontal, vertical, cardan/offset mounted, and machine trains.
1. Horizontal machine alignment
The most common alignment scenario involves two horizontally mounted machines, typically an electric motor driving a pump, fan, or gearbox. Laser systems are ideal for this setup. With a laser measuring unit mounted on each shaft, the system calculates shaft centerlines in real time, even while adjustments are made. The digital readout shows horizontal and vertical alignment values simultaneously, guiding the user through corrections with live feedback. This significantly reduces the time needed compared to traditional methods and ensures consistently high precision.
2. Vertical machine alignment
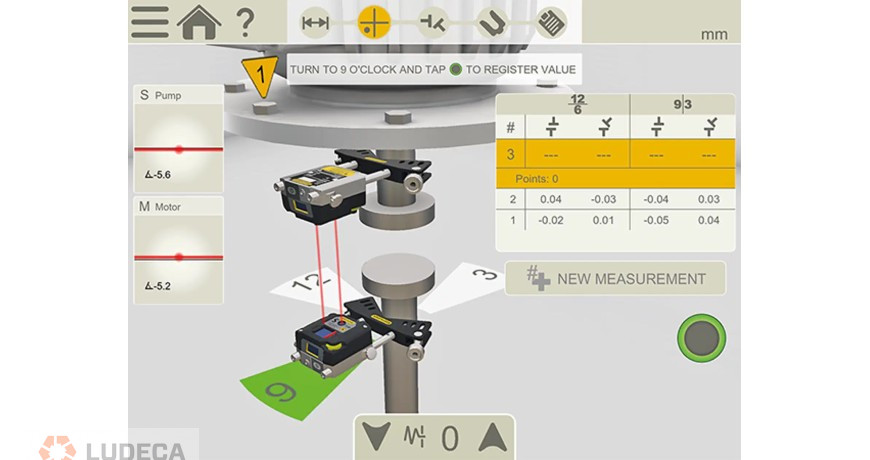
The vertical configuration is most common in pump applications, where the motor is mounted on top of the pump, often with a flange connection.
Vertical or flange-mounted motors present a different geometry, where the shaft rotates along a vertical axis. Alignment challenges often involve angular misalignment due to uneven flange contact or distorted mounting surfaces. The Easy-Laser systems include a dedicated vertical alignment program. It calculates center offset and angular deviation at multiple clock positions and provides adjustment values based on shims or repositioning. The result: fast and accurate alignment even when access is limited.
3. Cardan or offset mounted machine alignment
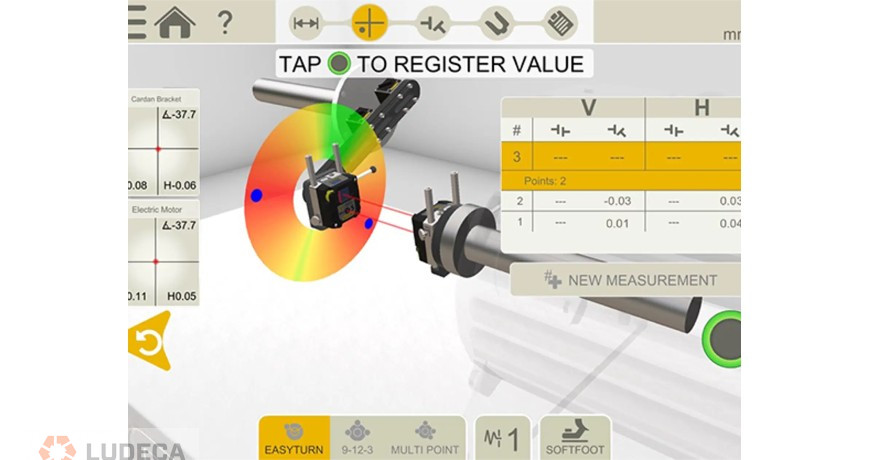
Some machines are connected via cardan shafts. These setups require the driver and driven shafts to be parallel, not colinear, making traditional alignment methods difficult. The laser system solves this by using a cardan shaft program that allows the user to align the motor based on angular and offset tolerances at defined measurement planes. With the cardan shaft temporarily removed, the laser measurement units are mounted on special cardan brackets and used to measure shaft positions. The system then provides adjustment values that ensure parallelism, accounting for angular twist and axial offset.
4. Machine train alignment
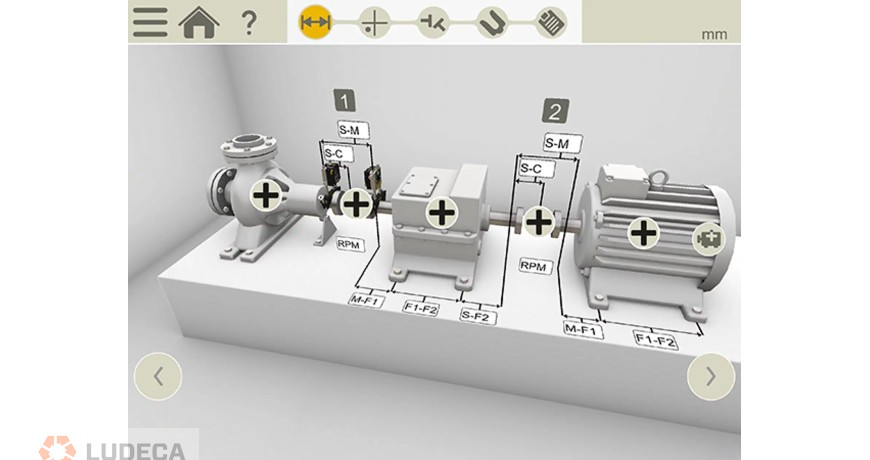
In multi-machine setups – such as a turbine driving a gearbox and generator, or a motor driving a pump and a compressor – proper alignment across all coupled machines is essential to prevent stress buildup and premature wear. Laser alignment systems simplify this complex task by allowing the user to build a virtual train model in the software. Each machine can be defined as fixed or movable, and the system calculates optimal alignment targets accordingly. Live adjustments can then be made at one or more positions, with results updated across the entire train in real time.
One tool, all configurations
By providing precise measurements, real-time feedback, and dedicated software functions for different configurations, the Easy-Laser systems streamline the alignment process and improve machine performance. Whether you’re maintaining a standalone pump and motor setup or a high-speed production line, investing in accurate alignment tools is always worth it.
Thank you Roman Megela with Easy-Laser for sharing this informative article with us!
by Diana Pereda
Repeatability: The degree to which a measurement process, procedure, or experiment returns the same results when said process, procedure or experiment is conducted over and over again.

Reproducibility: The degree to which all conditions affecting a measurement process, procedure or experiment can be duplicated from one execution to the next.
Accuracy: The degree to which a measurement process, procedure or experiment yields the truth.
“Repeatability does not accuracy make!” However, accurate readings should always be repeatable.
If repeatability is poor, but the process or tools used to obtain the measurement results is known to be good, then the cause of the non-repeatability (or repeatability outside of acceptable tolerances for deviation) must be poor reproducibility. For instance, if results don’t repeat, but you know your measurement tool is good and accurate (such as an Easy-Laser XT 770 Laser alignment system), there is a high likelihood of mechanical looseness (i.e. loose anchor bolts, or a loose bracket, or a loose rod in the bracket, or a loose coupling hub upon which the bracket is mounted), all leading to the conditions of the measurement not remaining consistent from one measurement to the next; alternatively, the conditions of the experiment are being affected by other external factors causing them to be continuously changing, such as machine temperatures cooling from a machine set that has recently been shut down, or the sun coming out from behind an obstruction and is now shining upon one machine but not the other, etc. etc.
Nevertheless, if reproducibility is good, and repeatability is good too, that still might not yield accuracy, because a repeatable error is intruding into the conditions of the experiment that compromises obtention of the truth. For instance, the laser head might be imperceptibly bumping or brushing against an obstruction to free rotation (such as a coupling stud in the base), or a protrusion of some sort (such as a bolt head protruding from the bearing housing), causing the laser head to be moved or deflected from its true position at rest just at that position, thereby compromising the truth of certain measurement points in the rotation. Thus, even though repeatable, the calculated results might still not “accurately” reflect the truth of the alignment, and these types of issues are particularly difficult to diagnose and pinpoint.
by Diana Pereda

The overhaul included extensive work on both the stator and rotor. With the mechanical work finished, the focus shifted to ensuring that the turbine could run reliably once it was restarted. Even small misalignment between the turbine and generator could lead to increased bearing loads, vibration, and long‑term reliability problems.
Getting the turbine ready for restart
Large turbine‑generator sets operate under demanding conditions, and installation accuracy is essential. After the overhaul, the shafts had to be aligned precisely to ensure smooth operation when the machine returned to service. Any deviation at this stage could introduce mechanical stress into the drivetrain and increase the risk of vibration or premature component wear.
Aligning the turbine-generator set
The alignment was carried out on a 237 MW Mitsubishi steam turbine-generator set using the Easy‑Laser XT770 laser alignment system. Magnetic brackets with offset extensions were installed so the measuring units could be mounted securely on the shafts.
The shafts were rotated using a crane, while digital inclinometers ensured that each measurement was taken at the same angular positions during each rotation. Using the Multi point program, three complete measurement cycles were performed to confirm repeatability and ensure reliable alignment data.

Accounting for thermal growth
Measurements were carried out under cold alignment conditions. Because machines of this size expand as they reach operating temperature, thermal growth had to be taken into account. In the XT Alignment software, thermal growth compensation values were added based on data from the machine’s technical drawings. This ensured that the turbine and generator would be correctly aligned not only during measurement, but also under real operating conditions.
Accurate alignment within tolerance
After completing the measurements and adjustments, the turbine‑generator set was aligned within tolerance and the final report was reviewed together with the maintenance manager and the team. It had been a demanding job, but the successful result, achieved through close cooperation between PEAK and the customer, made the effort worthwhile.
Why precise turbine alignment matters
Steam turbines are high‑speed machines and precise installation and maintenance is essential. Accurate shaft alignment plays a key role in plant availability, machine lifetime, and safe operation. For power plants, careful alignment is therefore not just a maintenance task – it is a key factor in ensuring stable and reliable power generation.
Thank you Easy-Laser for sharing this informative article with us!
Not All Vertical Turbine Pump Repair Shops Are Created Equal
by Diana Pereda
Anyone who has spent time in the field of machine repair has most certainly heard of “thermal growth”. This is the unavoidable act of materials expanding as they heat up or contracting as they cool down. Thermal growth is a well-known phenomenon that is dealt with extensively in alignment procedures. Components growing or shrinking with temperature change changes the offset and angularity of the shaft alignment and must be compensated for.
Thermal growth isn’t a concern for alignment crews only. It must be considered when setting up any machine or installing bearings on nearly any kind of machine. The reason for this is “Axial Growth” of a shaft. In other words, in addition to the radial positional changes caused by the expansion or contraction of the machine housings from thermal growth, the length of a shaft will also change with temperature changes.
If a shaft lengthens or shortens with temperature change, this must be considered when selecting the correct bearings to install on certain machines. Let’s break this down and give you a few things to consider before installing bearings on anything.
Consider the Temperature Change
The first question that must be asked is, how much temperature variation will the shaft be exposed to between the stopped, unloaded and ambient condition of the machine, and its fully loaded running condition? Some machines don’t see much variation at all. A good example of this would be a fan inside a climate-controlled office building or hospital. Other machines see drastic temperature variations. An example of those would be an oven circulation fan. When this machine is offline, the shaft is exposed only to ambient temperatures. But after being placed into service with heat in the oven, the shaft could be exposed to temperatures hundreds of degrees above ambient. The bigger the temperature changes, the more the shaft will grow and the more room the shaft will need to accommodate that growth.
What’s the big deal? Why worry about thermal growth?
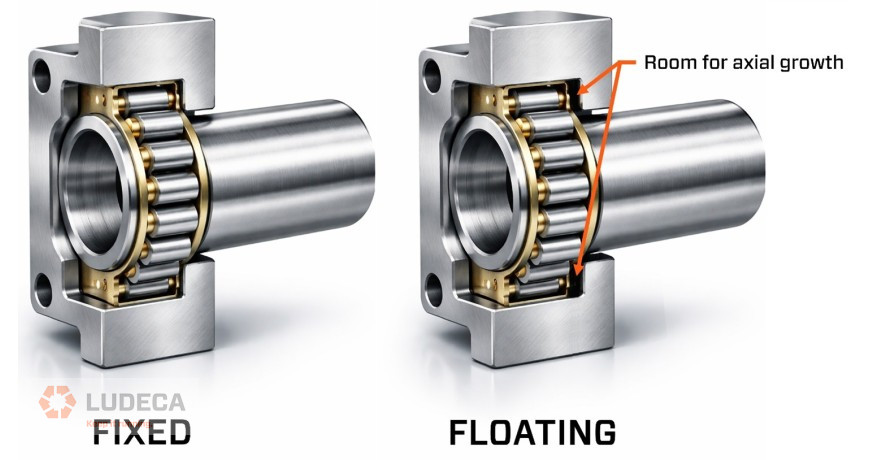
If we install two fixed bearings onto a shaft and bolt them down to a base, we have left nowhere for the shaft to go when it grows. In that case the shaft will bow or bend to accommodate its increased length, provoking potential imbalance vibration as well as unnecessary axial and radial loads on the bearings. This is where a floating bearing comes in. A shaft that experiences thermal growth should have one fixed and one floating bearing. The fixed will maintain the proper positioning of the shaft and the other will float inside its own housing, allowing the shaft to lengthen or shorten as needed. A shaft that is not allowed to lengthen or shorten freely will lead to excessive heat, vibration and premature failure.
How do floating bearings work?
A floating bearing has extra room inside the housing for the bearing to move in or out in the axial direction (ie. along the rotational axis of the shaft itself) as the shaft changes in length. The bearing is mounted to the shaft, and the housing is mounted to the base. The only thing that should move freely is the bearing inside the housing. The illustrations below show the difference between a fixed and floating bearing:
What kind of machines need Floating Bearings?
The simple answer to this question is any machine could experience significant axial growth of the shaft or of the machine housing that holds the bearings. It depends on the application and temperature variation. It is very important to remember the thermal growth rules for certain materials. Most shafts are made up of mostly carbon steel. However, some shafts are made up of stainless steel or other kinds of allows. Below is a chart of the most common alloys found in machines:
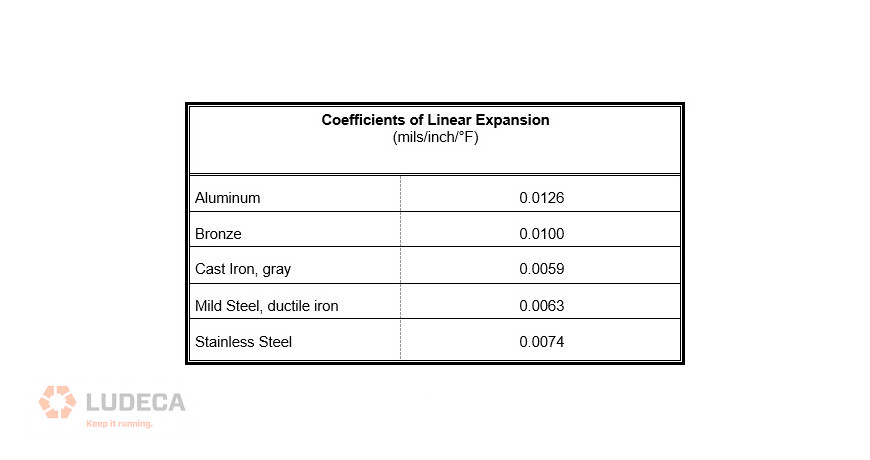
Formula for the calculation of thermal growth at the machine supports: T × L × C
Where:
- T = Change in Temperature (D°F).
- L = Distance of material involved (inches) (see Figure 16.).
- C = Coefficient of linear expansion (mils per inch of material per °F change in temperature)
This will tell you how much the material will grow per degree of temperature change.
Setting floating bearings, the right way
After deciding that a floating bearing is needed, the first thing we need to decide is which side of the machine should the floating bearing be mounted in? The drive end? Or the opposite drive end? There is no straight forward answer to that question. When placing the floating bearing on the drive end, you must consider either coupling gap, or belt alignment depending on how the machine is driven. Often times, it is better to place the floating bearing on the opposite drive end to avoid coupling gap or alignment issues.
However, the general rule of thumb when deciding where to locate the floating bearing is this: The floating bearing should be the one with the least amount of radial load. This allows the bearing to float freely without dragging and binding up. Sometimes it may be worth allowing some coupling float or sacrificing some belt alignment. Always use common sense and fully understand process parameters before making this decision.
The next thing we need to consider is, which way is the shaft or bearing going to go. In? or out? This depends on the temperature changes that the shaft will be exposed to when it is put into operation. If the shaft is going to be exposed to air or fluid that is hotter than ambient, we would want to locate the bearing favoring the inside of the housing to allow the shaft to grow. If the shaft is exposed to cold air or fluid, we would want to position the bearing toward the outside so the shaft can shrink. If extreme temperatures are expected both ways, it may be necessary to locate the bearing in the center of the housing. You must know the process to properly set up a floating bearing.
Conclusion
We hope this post has shed light on an often-overlooked issue. This is an issue that has destroyed bearings in their infancy more times than most would guess. Maybe now you can begin to set up machines to maximize working life. The goal is always to Keep It Running!
Watch our video Shaft Alignment Know-How: Thermal Growth to learn the importance of accounting for thermal growth on rotating equipment.
by Diana Pereda
Compressed gas is used everywhere. While there are several different types of compressors to pressurize gas, here we will talk about the reciprocating type which is widely used in all types of industry. Laser measurement and alignment of these types of compressors is essential both during the installation phase and to ensure reliable operation for many years.
Compressor package installation
Manufacturers of large reciprocating compressors have clear guidelines for how the equipment should be installed and maintained for best performance. And with laser alignment equipment, you can perform 90% of the measurements that are required:
- Measure flatness and level of foundation and compressor and driver sole plates.
- Check soft foot of compressor and driver.
- Perform shaft alignment between driver and compressor.
- Perform bore alignment verification:
– Measure flatness and level of the top plane of the compressor frame.
– Check main bearing and connecting rod bearing clearance.
– Check connecting rod and crankshaft thrust clearance.
- Measure engine thrust.
- Perform dynamic measurement to check thermal expansion and pipe strain.
- And more.
All this can be done with a single system, the Easy-Laser® XT770 Shaft+GEO, which gives the technician full control of the whole process. After installation you need to perform these checks with regular intervals.
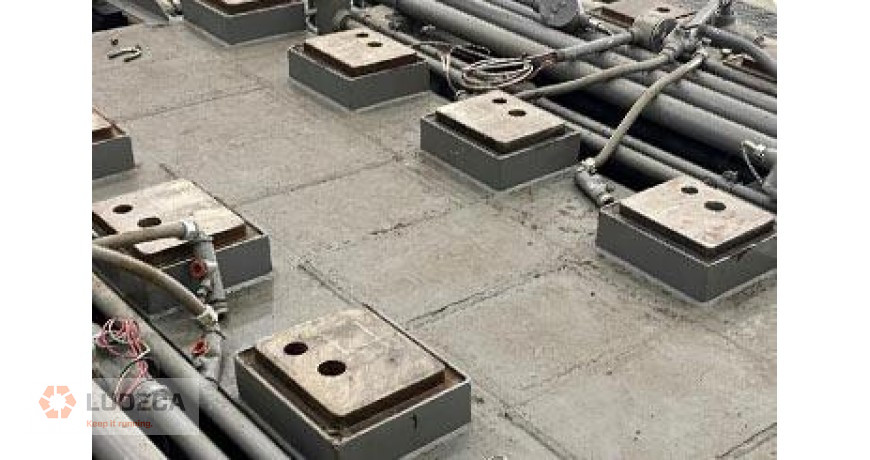
Foundation flatness and level
For any machine that contains rotating parts, it is essential that the foundation on which the machine is placed is completely flat and level. To perform this type of measurements, the Flatness program should be used together with the XT20 or XT22 laser transmitter and the XT70 measuring unit.
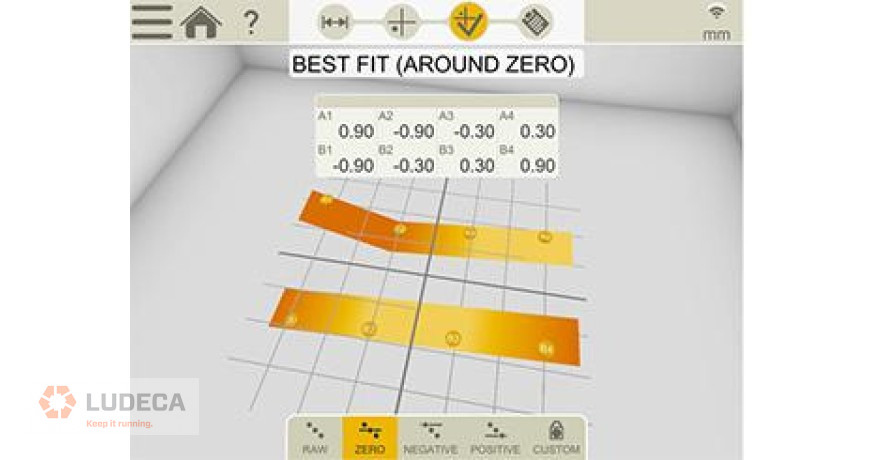
Soft foot check and shaft alignment
Soft foot is a condition that must be avoided, since it can cause great damage to bearings, shafts, and other parts of the machine. The occurrence of soft foot can be detected within the Shaft alignment program. Once you have checked and taken the necessary action to fix any soft foot problem, shaft alignment between the driver and compressor can take place using the XT770 shaft alignment equipment. Learn more: The four different types of soft foot.
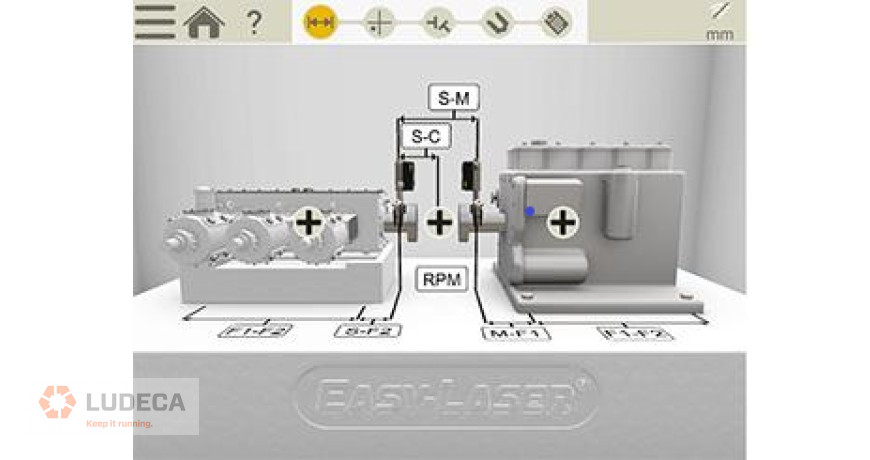
Main bearing bore alignment
The mounting surface of the top cover on a compressor frame is precision-manufactured to be flat and aligned with the main bearing bores and the bottom of the compressor feet. To ensure the best running conditions for the compressor main bearing and crank shaft, it is important to measure this surface, so it is aligned within the recommended tolerances.
The mounting surface essentially consists of two rails which are measured using the XT20 or XT22 laser transmitter and the Flatness program (the same as when measuring the foundation). The number of points you need to measure is determined by the compressor manufacturer.
Checking of clearance and thrust
Bearing clearance refers to the space between the shaft and the bearing surface which is filled with lubricating oil. It’s important to keep this within tolerance to avoid bearing failure. On the compressor, we need to measure the main bearing clearance and the connecting rod bearing clearance. The clearance space is measured by lifting the shaft/rod and measuring the gap.

We also need to check that there is no excessive thrust in the crankshaft or connecting rod, which could cause serious damage to bearings, pistons, or other components. We do this by measuring the horizontal movement. We mount the detectors, set them to zero and then by using a prey bar, we force the crank shaft to move axially to its end. Then we record the travel which is our clearance. Engine thrust is measured in the same way.

Measure machine movement
A dynamic measurement is conducted while the machine is running, to check whether there are any external forces that can have a negative effect on machine performance. This can be for example pipe strain or thermal growth. A dynamic measurement check is done using special brackets and the EasyTrend program. The brackets are placed on the machine and measurement values are recorded during a set period of time. This will reveal if there is any unwanted angle or offset movements that need to be corrected.
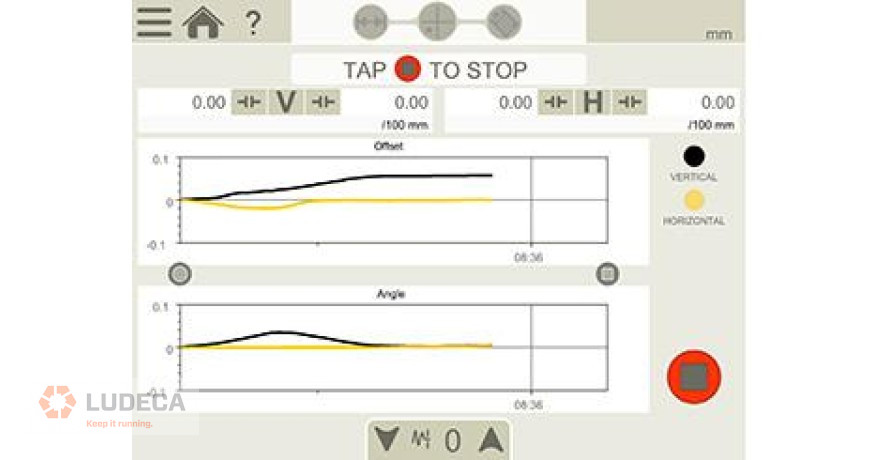
Continued maintenance for optimal performance
Once all measurements and adjustments have been made and the compressor is up and running, it is important to establish a routine for regular maintenance. Large compressor manufacturers recommend that you perform bore alignment verification, engine thrust measurement, shaft alignment and dynamic measurement every 4000 hours. And every 8000 hours you need to do an even more thorough check. Be sure to always follow the manufacturer’s recommendations. And if you have any questions, don’t hesitate to contact us!
Thank you Roman Megela with Easy-Laser for sharing this informative article with us!
A Before and After of Alignment on a Caterpillar Engine mated to an Ariel Compressor
by Diana Pereda
A while back, a German company that provides gas contacted Easy-Laser GmbH to participate in the troubleshooting of a machine that showed high vibrations levels. The machine was a geared compressor supplying nitrogen gas for the process. As part of the investigation, the compressor owner asked us to provide thermal compensation values for the alignment.
We got access to the report from the last shaft alignment job, where we could see that thermal compensation was applied.
Our plan for this investigation was to start by checking the shaft alignment status in cold conditions when the machine was standing still, in a non-operating state. And the results from this shaft alignment check revealed that the machines were misaligned more than twice the amount of the specified thermal compensation value in the vertical position.
We then installed laser sensors on the motor and the compressor to perform what is called a dynamic measurement (this is done using special brackets (see illustration below) and the alignment program EasyTrend).

We started the compressor and began to measure its dynamic movements. First, we performed a dynamic measurement until the machines reached operating temperature. Then we turned the machines off and performed shaft alignment verification in hot condition. Afterward, we mounted the sensors back on the machines again and measured the movement from hot to cold conditions.
We basically performed 4 measurements:
- Shaft alignment verification in Cold condition.
- Dynamic measurement from Cold to Running.
- Shaft alignment in Hot condition.
- Dynamic measurement from Hot to Cold condition.
The results:
The shaft alignment made during Cold condition revealed that thermal compensation values had been inserted into the alignment protocol, but they were more than doubled! A wrong interpretation of the compensation values or other mistakes must have occurred when the machines were aligned in the past.
The dynamic measurement from Cold to Running conditions revealed that the compressor movement in the vertical position, due to thermal expansion, was exactly the same as the specified thermal compensation value provided by the compressor owner. But, since that value was doubled, the compressor was heavily misaligned in the vertical direction. To our surprise, we found out that the compressor moved 1,3 mm in the horizontal position, which nobody expected. Horizontal misalignment of 1,3 mm is very severe.
The dynamic measurement from Hot to Cold conditions confirmed the values and direction of the movement while the compressor was cooling down.
Conclusion:
Do not assume that the calculated value for thermal compensation is correct and the machines are compensated for it correctly. Instead, measure your machines, check the alignment conditions, and verify.
Watch our Shaft Alignment Know-How: Thermal Growth video to learn the importance of accounting for thermal growth on rotating equipment!
Thank you Roman Megela with Easy-Laser for sharing this informative article with us!
by Diana Pereda
Not too long ago, I was called out to balance a supply fan on an air handler at the local zoo. I arrived on site and immediately noticed the heavy vibration coming from the air handler. I collected some vibration readings, shut the machine down, and locked it out. After looking through the vibration data and some visual inspection, I was able to rule out unbalance as the primary source of the vibration. The motor and fan bases on this belt-driven machine were in rough shape: loose and missing hardware, isolators worn and out of adjustment, and machine mounted to a weak foundation. These issues certainly made the vibration worse and needed to be addressed, but they were not the source of the vibration.
After performing a number of tests and checks, I found that the vibration was caused by a combination of sheave misalignment and an overly tensioned belt. After speaking with the customer, I found out that the belt and sheaves had just been installed the day before! Unfortunately, many millwrights and mechanics fail to have the training, tooling, or desire to properly align and tension a belt-driven machine. Taking the time to understand how and why to perform sheave alignment and how to properly tension a belt drive can save thousands on repair costs, increased efficiency, and unscheduled downtime. In addition, reliability is especially critical when in a medical or veterinary application, such as was the case in the example above. Below we will discuss how sheave alignment and belt tension affect the machine, as well as some best practices to get the job done and #keepitrunning.
Effects of Poor Sheave Alignment and Belt Tension
- Belts Too Tight: An overly tensioned condition will cause excessive radial load on the shafts and bearings, as well as an added electrical load on the motor. It will lead to misalignment during operation (deflected shafts), decreased motor life, decreased shaft life, premature wear on bearings, and an overall loss of efficiency.
- Belts Too Loose: A loose condition will cause belt slippage, and in turn, overheating. It will lead to a significant loss in efficiency, premature wear on belts and sheaves, and, through heat transfer, can decrease the life of the bearings and motor.
- Sheave Misalignment: Sheaves out of alignment will cause many of the same issues as an improperly tensioned belt, including overheating, slippage, and excess radial load. More specifically, misaligned sheaves will cause heavy vibration, as well as premature and uneven wear on the belts and sheaves.
Best Practices for Sheave Alignment and Belt Tensioning
- Sheave alignment and belt tensioning should be done somewhat simultaneously. The alignment process will affect the belt tension and vice versa. Don’t assume it’s in spec, check it!
- Install sheaves as close to the bearings as possible or reasonable. This reduces the load on the shaft and bearings by reducing the potential for shaft deflection.
- Check shafts and sheaves for runout before performing the alignment. Runout can cause many issues, including making alignment and belt tensioning more difficult.
- The closer the span between the motor sheave and the driven sheave, the more sensitive the machine will be to misalignment or improper belt tension. A longer span will be more tolerant. Machine speed will also play a factor. The higher the RPM, the more wear over a shorter amount of time. Keep this in mind.
- Check sheaves for wear using a sheave gauge. Gaps 1/16″ or larger indicate a sheave is worn and should be replaced. A belt will have a hard time gripping a worn sheave, which will translate into slippage and excessive heat.

- Use a sheave gauge to check sheaves for excessive wear.
- Check belt tension using a pencil gauge (with corresponding belt tension spec chart) or a frequency meter. Both methods are accurate and easy to perform if done correctly. In general, you should tension belts as follows: using a spring scale, press down on the belt in the approximate center of its span (on the tight side), to deflect the belt 1/64″ per inch of span length and observe the force required to do so. If you are not sure of the belt span length you may also use the center-to-center distance of the pulleys, which will be similar. Tension the belts until the force required for this deflection equals the belt manufacturer’s maximum recommended force values for the specific belts you are using. Make certain this force does not exceed the machinery’s design loads. The force values for all belts should fall within 10% of each other.
- You can align the sheaves using a cord, but the quickest and most accurate way is a laser pulley alignment tool such as the Easy-Laser XT190. The XT190 works for all types of belt drives, as well as chain drive applications. The benefits of seeing offset, angularity, and twist simultaneously on the screen, while being able to make live adjustments, makes sheave alignment with the XT190 quick, easy, and accurate.
Does It Make a Difference?
In the scenario above the difference between a heavy vibration and a smooth running machine was a slight alignment adjustment and 2 lb. reduction in belt tension. That’s it! When it comes to installing and maintaining industrial machinery, the devil is in the details. Don’t assume it’s right, know that it is using knowledge and the proper tools available.
Download our 5-Step Sheave Pulley Alignment Procedure for a simple and effective procedure for sheave pulley alignment of belt-driven equipment!
by Diana Pereda
In almost every heavy industry, you will find rotating machinery. You could say that rotating machinery makes the industrial world go round. Unless, of course, it doesn’t.
When rotating machines go awry, it can be nothing less than catastrophic. At the very least, when there is misalignment, the result is unwanted heat, noise and vibration, as well as an increase in fuel usage, a shortening of the lifespan of components and potentially the need to shut down operations and replace or repair key mechanisms. As a snapshot, rotating machines that need precise alignment to function optimally include crankshafts and camshafts within internal combustion engines, pumps, compressors and centrifuges in the process industry, wind turbines in the renewable energy industry, and an enormous variety of machines within the automotive, marine and manufacturing sectors. The business case for ensuring optimum operational levels is crystal clear, yet even businesses with many years’ experience using rotating machinery will sometimes cut corners – and almost always to their cost.
Prioritizing productivity
Given the high level of engineering built into modern industrial equipment, productivity gains have tended to become increasingly incremental, with far fewer opportunities for innovative leaps forward. With this in mind, operational methodologies are now under closer scrutiny, with best practice being the primary focus of efforts to extend service intervals and maximize machine uptime.
Roman Megela is the senior reliability engineer with Easy-Laser, a company that produces laser-based alignment solutions for rotating machines across a variety of industries. He is very clear – not to say evangelical – about the importance of maintaining alignment within these machines. “In the case of machine installation,” he says, “it is crucial that the machine is installed on a flat and levelled foundation. It is a must to measure and verify the foundation to avoid distortion of the machine’s casing. If this is not addressed during the commissioning phase, the machine’s operational life will be reduced, by perhaps as much as 50%, from the very start. Also, at some point, misalignment will cause the machine to fail and it will need to be repaired, with the additional expense of technicians having to re-install it.”
Precision in compression
One area in which Megela is seeing an increasing need for both improved performance and greater machine lifespan is compressed gas systems; in particular reciprocating compressors. When it comes to maximizing their performance, he says, “precision is key – especially during the setup phase.” Manufacturers generally provide strict guidelines on how reciprocating compressors should be aligned and checked, and Megela says this is where laser measurement tools really come into their own, being able to take care of perhaps 90% of the required checks.
“That includes everything from making sure the foundations and base plates are flat and level, to checking for soft foot, aligning the shaft between the driver and compressor, and verifying internal alignment like bearing clearances and thrust settings,” he says. On top of that, he says, dynamic checks can be made, including tests for thermal expansion and pipe strain, “because over time, those can significantly affect performance.”
“Ideally, it should all be done with one system, ensuring the process remains consistent. And it’s not just a one-time thing. After installation, you need to recheck everything regularly to make sure the machine keeps running the way it should.”
Stability means sustainability
Megela is a great believer in prevention being better than cure and he travels the world, explaining to engineers and technicians that the correct alignment of machinery could literally add years to its lifespan, benefitting not only the company’s bottom line, but potentially the planet too. He explains that, in the last five years, the industry has changed dramatically in the face of a number of different challenges, “from Covid, through components shortage, then energy prices going through the roof. If you add the cost of downtime, which includes loss of production, plus maintenance costs, it makes it very difficult for a business to have money to invest in new assets. Every organization I speak to is trying to become more efficient and sustainable, utilizing their available resources. It’s true that every machine has to be overhauled at some point, but this should as much as possible be a planned event, not due to failure. If you can manage this, you can potentially extend the life of your machine by ten times – then you’ve opened the door to serious sustainability.”
In fact, Megela sees it very much as being at the heart of his role, to educate industry professionals about the benefits of greener operations. “Sustainable practices will help to cut down maintenance costs and keep machines running,” he explains. “That translates into reliable operation which can also have a major impact on the return on a company’s investment.” This seems to be common sense, but Megela says he has visited companies for whom components that should last for a number of years, are regularly being replaced within 12 months, due more often than not to a failure to check alignment. The result is unplanned downtime for machinery, and potentially the need to bring technicians in to carry out unplanned maintenance. If the machine happens to be on a ship, or an offshore oil rig, transportation and travel costs can rise exponentially.
An all-industry issue
On the complexity of some of the maintenance and repair processes, Megela says, “It’s always time-consuming to stop production, drain and purge systems, lock out and tag out machines.” He adds that, due to the complexity of their processes, businesses within the refining, chemical, petrochemical and energy production industries are likely to suffer the most when misalignment strikes. “It needs to be understood that alignment is a condition, not a task,” he says. “Keeping the alignment condition within the tolerances is the key to maximizing your overall uptime and the benefits of alignment are huge. Bearings will operate under designed loads, lubrication will remain unchanged, no strain will be added to the shafts, mechanical seals and couplings.”

Megela says some of the companies he visits are surprised at how regularly checks on alignment are required. He says, “We should check the alignment after the installation every three months. Only after nine months of repeating solid values should we start extending verification periods to up to two years. In this way, the life of a machine can be significantly extended, with the potential for huge long-term financial benefits.” Regular inspections of equipment will almost certainly identify a problem, as rotating machines will immediately respond to misalignment, with increased vibration, temperature, energy consumption and noise, and potentially leaking seals and compression capacity drop.
“When misalignment is identified, a plan for correction must be presented and acted upon, before there is potentially a catastrophic failure of the asset. Cutting corners at this point is always disastrous; there is nothing more economical than a perfectly aligned machine. The result is a long service life and minimal component wear and tear; that means a saving on replacement parts – a saving on natural resources, as well as the consumption of less energy. This is one of the ways we ensure industry becomes more sustainable.”
Thank you Roman Megela with Easy-Laser for sharing this informative article with us!
by Diana Pereda
Guest post by John Lambert at Benchmark PDM
Recently I have been seeing the P to F interval curve popping up a lot on my LinkedIn feed and in articles that I have read. It was a concept that I was first introduced to when I was implementing Reliability Centered Maintenance into the Engineering and Maintenance department at the plant where I worked at the time. It was a great idea, that if done correctly is a maintenance benefit. Why, because it’s cost savings and cost avoidance. Let me explain this.
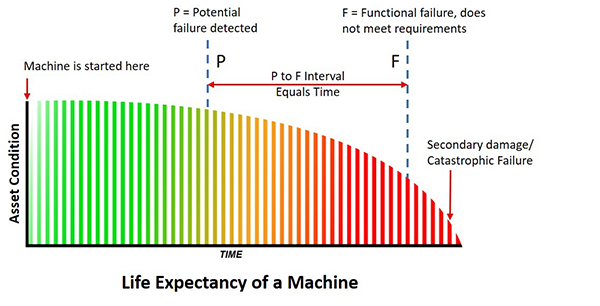
The P to F curve was used as a learning tool for Condition Based Maintenance. The curve is the life expectancy of a machine, an asset. The P is the point when a change in the condition of the machine is detected. The F is when it reaches functional failure. This means that it is not doing the job it was designed to do. For example, if it were a seal that is designed to keep fluids in and contamination out and is now leaking, it’s in a state of functional failure. Will this put the machine down? Probably not, but it depends on the importance of the seal and the application. This is an important point because the P (potential failure) is a fixed point when you detect the change in condition but the F (failure) is a moving point. Not all warnings of failure put the machine down very often you have options and time. Consider this: If I have a bucket that has a hole in it, it is in a functional failure state. But can I still use it to bail out my sinking boat? You bet I can!
Failure comes at us in many ways and obviously, we have many ways to combat it. If you detect the potential failure early enough (and it can be months and months before actual failure) it means that you can avoid the breakdown. You can schedule an outage to do a repair. It’s not a breakdown, the machine hasn’t stopped, it’s no downtime. This is cost avoidance and the plant can save on the interrupted loss of production because of downtime costs.
There are a lot of examples of cost avoidance and also of cost savings. For instance, at the plant I worked at we used ultrasound to monitor bearings. We detected a very early warning in the sound level and were able to grease the bearing and the sound level dropped. We saved the bearing of any damage, and we saved a potential breakdown so this is cost savings. Even if there is some bearing damage, the fact that we are aware of and monitor the situation lets us avoid any secondary damage.
It’s one price to replace a seal and it’s more if you have to replace a bearing in a gearbox. However, it can be very expensive to have to replace a shaft because the bearing has sized onto it and ruined it. Secondary, ancillary damage can mount up very quickly if you don’t heed the warning you are given with the P of potential failure. This warning of potential failure gives you time before any breakdown. The earlier the detection, the more time. Time to plan, and view your options. And what people tend not to do is failure analysis while the machine is still in service. A failure analysis gives you a great start on seeking out the root cause but starts right away, not when the machine is down.
Condition monitoring or as it’s often called Condition-based maintenance (CBM) does work. However, for me, there is a downside to this and I will explain why shortly. CBM is based on measurement, which is good because we all know to control a process we must measure.
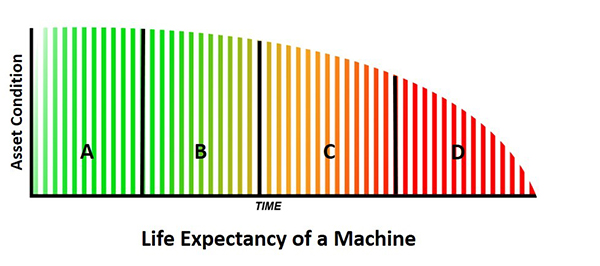
Consultants (and I’m guilty) like to put labels on things and you may see:
1. Design, Capability, Precision Maintenance
2. CBM, Predictive Maintenance
3. Preventive Maintenance
4. Run to Failure, Breakdown Maintenance
For me, the P to F interval curve starts when the machine starts. That means Design and Precision Maintenance is not in the curve and this happens before startup. A small point but it takes away from the interval meaning.
We use predictive maintenance technologies in CBM. Vibration, Ultrasonic, Infrared, Oil Analysis, NDT (i.e. pipe wall thickness), and Operational Performance. They are all very good technologies, yet it is a combination of cross-technologies that works best. As an example, vibration may give you the most information yet ultrasound may give you the earliest warning on a high-speed bearing. And then there is oil analysis which may be best for a low-speed gearbox. It all depends on the application you have which dictates what’s best for you. A lot of time and effort was placed on having the best CBM program and buying the right technology.
This, I believe, lead to the maintenance departments putting the focus on Condition-based maintenance! This I think is wrong because we still have failure. This means that CBM is no better than Predictive Maintenance. This doesn’t mean that I don’t recommend CBM, I do. To me, it’s a must-have but it does not improve the maintenance process because you still have machine failure. Machine failures fall into three categories Premature failure, Random failure, and Age-related failure. We want the latter of these. We know from studies that say that 11% of machine assets fail because of age-related issues. They grow old and wear out. This means that 89% fail because of some other fault. This is a good thing because it gives us an opportunity to do something about them.
These numbers come from a very famous study by Nowlan and Heap (Google it!) that was commissioned by the US Defense Department. It doesn’t mean these numbers are an exact reflection of every industry but the study but it has stood the test of time and I believe it has led to the development of Reliability Centered Maintenance. But let’s say it’s wrong and let us double the amount they say is age-related (full machine life expectancy). That would make it 22% and 78% would be the number of random failures. Even if we quadruple, it’s only 44% meaning random is at 56% and we are still on the wrong side of the equation. The maintenance goal has to be to get the full life expectancy for all their machine assets.
In order to get the full life expectancy for a machine unit, I think you have to be assured of two things. One is the design of the unit which includes all related parts (not just the pump but the piping as well). The other is the installation.
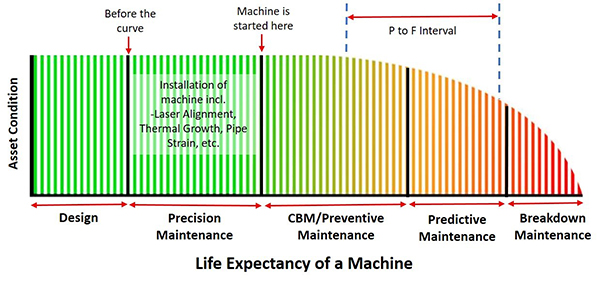
If you’re like me, and you believe that Condition Based Maintenance starts when the machine starts then you understand that there is a section of the machine’s life that happens before. You could make an argument that it starts when you buy it because, as we all know, how we store it can have an effect. However, what is important at this stage is the design and installation of the machine. In most cases, we do not design the pump, gearbox, or compressor but we do size them so that they meet the required output (hopefully). We do quite often design the piping configuration or the bases for example. All of which is very important but the reality is that maintenance departments maintain already-in-place machine assets. So, although a new installation, requiring design work is not often done, installation is. Remove and Refit is done constantly. And the installation is something that you can control. In fact, it’s the installation that has the largest influence on the machines’ life. The goal is to create a stress-free environment for the machine to run. No pipe strain, no distorted bases, no thermal expansion, no misalignment, etc.
Precision Maintenance was a term I first heard thirty years ago. It’s part of our M.A.A.D. training program (Measure, Analyse, Action, and Documentation). It’s simple, it means working to a standard. Maintenance departments can set their own standards. However, all must agree on it and adhere to it. This is the only way to control the installation process. This is the way to stop random failure and get the full life expectancy for your machine assets. The issue is that we do not have a general machinery installation standard to work to. Yes, we can use information from other specific industry sources such as the American Petroleum Institute (API) or the information from the OEM (both of these are guidelines) however nothing for the general industry as a whole. Well, this is about to change. The American National Standard Institute (ANSI) has just approved a new standard that is about to be published. I know this because I worked on it and will be writing about it shortly.
If you look at the life cycle of a machine, we need to know and manage the failure as best we can. If we only focus or mainly focus on the failure, we will not improve the reliability of the machine. We cannot control the failure. What we can control is the installation and done correctly this will improve the process giving the optimum life for the machine.
I sell laser alignment systems as well as vibration instruments. If a customer were to buy a vibration monitoring tool before they bought a laser system. I would think their focus is on the effect of the issue, not the cause. What do you think?
by Ana Maria Delgado, CRL
In industrial settings, rotating equipment such as pumps and motors demands exact alignment to operate efficiently around the clock. A frequent installation flaw—soft foot—occurs when machine feet fail to contact a flat foundation uniformly, or pipe strain exists, causing machine frame distortion that misaligns critical components such as bearing bores. This twisting or bending of the machine frame undermines the precision of machined internals, leading to vibration, wear, and inefficiency. Correcting soft foot is straightforward and vital, preventing these issues and ensuring long-term performance.
Why Flatness Matters: ANSI/ASA Guidance
Machine feet are designed coplanar and flat for stable mounting. Uneven bases introduce undesirable distortion. Per ANSI/ASA S2.75-2017, baseplate flatness (coplanarity) is paramount, requiring less than 2 mils of spacing between feet. Flatness directly affects shaft alignment; verify it first using a straightedge or dial indicator before installation.

Streamlined Correction Process
- Shim for Contact: Fill foot gaps with shims, limiting to 3–4 per foot for rigidity.
- Rough Alignment: Install the machine and achieve perform rough shaft alignment.
- Soft Foot Check: Use your laser alignment tool’s soft foot program, such as that in the intuitive Easy-Laser XT series, to provide clear graphical feedback on bolt adjustments. It identifies distortions in real time, guiding precise corrections without trial and error—this step is typically needed only once.
Valuable Resources
For practical insights, LUDECA’s free Soft Foot Find-and-Fix Infographic and 5-Step Shaft Alignment Procedure offer clear visuals and steps to implement effectively. These tools simplify detection and resolution, enhancing installation outcomes.
by Diana Pereda

Misaligned pulleys are one of the most common, and costly, causes of belt-driven machinery problems. Yet pulley alignment is often overlooked in regular maintenance routines.
What is pulley alignment?
Pulley alignment is the process of ensuring that pulleys (sometimes also referred to as sheaves) in a belt-driven system are positioned correctly relative to each other. The laser belt alignment tool projects a laser line that runs parallel to one pulley. This line acts as a reference to align the other pulley.
The benefits of pulley alignment
Whether in manufacturing, HVAC systems, or marine applications, proper pulley alignment can significantly improve performance, reduce wear, and save energy. Below, we explore the main benefits of pulley alignment and why it’s worth investing in accurate alignment tools.
Reduced energy consumption
When pulleys are misaligned, the belt doesn’t run smoothly. Instead, it slips, bends, or rides unevenly, which increases friction and resistance. This extra load forces the motor to work harder, consuming more energy.
Even small misalignments can lead to surprisingly large losses. A case study showed that proper pulley alignment can reduce energy consumption by up to 20 percent – a saving that quickly adds up in systems running 24/7.
Extended belt and pulley life
Misalignment causes uneven tension and side loading on belts, which leads to premature wear or even breakage. Heat generated from high friction will also degrade the belt material over time. The pulleys themselves also suffer, developing irregular wear patterns that eventually require costly replacement.
By aligning pulleys correctly, you ensure even load distribution, reduce vibrations, and minimize belt tracking issues. This extends the service life of both belts and pulleys and reduces the need for unplanned downtime.

Improved machine reliability
Poor alignment doesn’t just affect the belt drive. It can introduce vibration and stress that travels through the machine, affecting bearings, couplings, and connected components. Over time, this can lead to serious breakdowns and costly repairs.
Proper pulley alignment improves machine stability and reliability. You get fewer unexpected breakdowns and more predictable maintenance intervals with regular alignment checks.
Faster and safer maintenance
Alignment using straightedges or string can be time-consuming and there is always the risk of human error. Laser alignment tools eliminate guesswork by providing clear visual feedback and live digital readouts. Unlike traditional methods, they allow you to check alignment in both horizontal and vertical planes simultaneously, without rotating components or needing extensive disassembly. One technician can perform the job accurately in a fraction of the time. The result is faster alignment, fewer errors, and safer working conditions.
A smart investment with lasting returns
When you add up the energy savings, extended component life, reduced downtime, and faster maintenance, the total cost of ownership for belt-driven equipment drops significantly. In short, pulley alignment matters more than you might think, and even a small adjustment will bring measurable returns. And investing in a laser alignment tool like the Easy-Laser XT190 Belt Alignment Tool quickly pays for itself through these ongoing savings, especially in operations with multiple belt-driven machines or high uptime requirements.
Download our 5-Step Sheave Pulley Alignment Procedure for a simple and effective procedure for sheave pulley alignment of belt-driven equipment!
Thank you Roman Megela with Easy-Laser for sharing this informative article with us!
Align Your Belt or Chain-Driven Machines with Modern Laser Belt Alignment Systems!
by Diana Pereda
Some coupling manufacturers will sell couplings claiming that the coupling can take a large amount of shaft misalignment. While this is true for most good quality flexible couplings, this capability can be easily misinterpreted. Flexible couplings are designed to withstand, without damage, some shaft misalignment. Sometimes it is perceived that, since the coupling can take the misalignment, the machines can run under this condition without any consequences. When running machinery with significant shaft misalignment, bearing and seal life will be impacted, resulting in premature failures along with other types of machine damage. This difference is not due only to coupling manufacturers’ generosity; there is a valid mechanical reason for building flexible couplings that can withstand much more misalignment than what is good for the machinery they connect: this “extra” misalignment capacity allows certain machines to be deliberately misaligned in the unloaded “cold” and stopped condition to allow for the changes that will occur in the alignment as the machines are set to run and arrive at the fully loaded “hot” and running condition, and account for dynamic load shifts as may occur. This deliberate misalignment is called alignment to target specifications, and LUDECA offers a number of ways of determining what these might be. If the good quality flexible couplings would not have this additional misalignment capacity, some machines could never be “short coupled” together and would require a long spacer shaft between them to allow for the thermal growth or dynamic load shifts. Now then, with that said, we reiterate that the fact that a good coupling allows for lots of misalignment is never an excuse for you to allow such excessive misalignment to exist between your machines in the running condition.
The table below shows some key differences between the two sets of tolerances.

Therefore, for longer machinery life, it is always recommended to have the equipment laser aligned to standard industry tolerances such as (ANSI/ASA S2.75-2017), and not to the looser alignment tolerances allowed by the coupling manufacture itself. See tables 2 & 3 below.
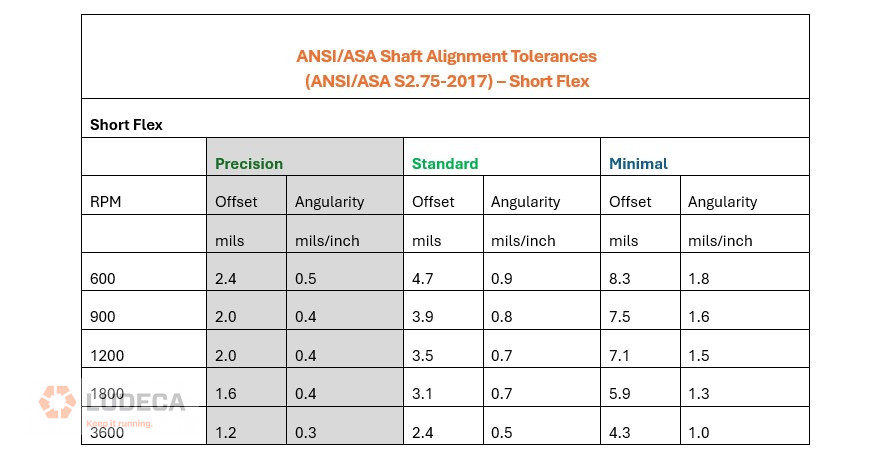

Are Coupling Manufacturer Tolerances Good Enough for Shaft Alignment?
by Diana Pereda